Under the industrial backdrop of New Energy Vehicles (NEVs) fully advancing toward “large-component lightweighting” (such as 6,000T to 16,000T integrated die-cast rear underbodies and battery packs) at “structural high-strength steel adoption” (such as hot-formed steel and third-generation advanced high-strength steel), metal melting and temperature control accuracy are facing unprecedented engineering limit challenges.
Whether dealing with large-tonnage melting-holding integrated furnaces for aluminum alloys or vacuum/induction melting equipment for high-strength steel, even minor temperature control deviations (within ± 5℃ ) can be linearly amplified, leading to the scrapping of vehicle castings or the failure of critical safety components.
I. Extreme Temperature Control Challenges in Melting Ultra-Large Cast Aluminum Components (Integrated Die Casting)
Ultra-large aluminum alloy die-castings (such as integrated vehicle body-chassis structural parts) typically utilize Al-Si-Mg series alloys (hal., AlSi10MnMg). Due to large wall thickness variations, complex structures, and extremely long processing chains, these castings impose rigorous demands on melt quality, presenting the following bottlenecks for induction furnace temperature control:
- “Electromagnetic Stirring-Temperature Field” Coupling Imbalance in Large-Capacity Melt Pools: As furnace capacity jumps to the multi-ton level, the alternating electromagnetic field generated by medium-frequency induction furnaces accelerates alloy composition homogenization but also induces violent electromagnetic stirring. Excessive power or mismatched frequency causes turbulent surface rolling, accelerating hydrogen absorption in the aluminum melt (forming pinhole defects) and burning losses of active elements like magnesium and strontium; insufficient power leads to upper-lower temperature layer separation and localized supercooling or superheating at the bottom.
- Temperature Sensitivity of Eutectic Silicon Nucleation and Secondary Dendrite Arm Spacing (SDAS): The pouring temperature window for aluminum-silicon alloys is typically strictly restricted to a narrow range (hal., 680℃ ± 5℃ ). Excessive temperatures exacerbate iron-phase precipitation and grain coarsening, while low temperatures trigger sudden drops in fluidity, cold shuts, or incomplete fill defects.
- Volatilization Threshold Control of Trace Modifier Elements: Modern automotive body aluminum alloys heavily rely on Ti-B master alloy refiners and strontium (Sr) modification. In high-temperature induction melting, for every 10℃ increase in temperature, the oxidation and burning rate of strontium increases non-linearly, directly leading to major fluctuations in mechanical properties (elongation and tensile strength).
II. Precision Temperature Control Requirements for Melting and Heat Treatment of High-Strength / Ultra-High-Strength Steel
During the melting stage of ultra-high-strength steel (such as 1500MPa to 2000MPa grade hot-formed steel) used in NEV crash beams, A/B pillars, and battery explosion-proof floor panels, chemical composition and purity control reach trace levels:
- Temperature-Chemical Dependency of Carbon, Manganese, and Silicon Alloy Balance: Minor temperature fluctuations during induction melting or induction through-heating of high-strength steel alter carbide dissolution equilibrium, austenitization rates, and the floating dynamics of deoxidation products (such as Al₂O₃ and inclusions).
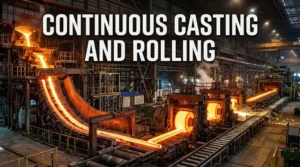
- Superheat and Inclusion Control: Molten steel superheat directly determines the solidification structure of continuous casting blanks or ingots. Excessively high temperatures easily aggravate the erosion of refractory materials (such as magnesia-dolomite or spinel linings), introducing foreign refractory inclusions; excessively low temperatures fail to effectively remove micro-oxide inclusions, which become fatigue crack sources during subsequent stamping and service.
III. Underlying Technical Bottlenecks Facing Medium-Frequency Induction Furnace Temperature Control Systems
- Dynamic Lag of Non-Linear Impedance and Thermal Inertia: During the phase transition process of the induction furnace from cold charge melting to liquid holding, the magnetic permeability (especially the Curie point transition of steel) and resistivity of the charge vary drastically with temperature, causing real-time drift in the load equivalent impedance. Traditional PID algorithms easily produce overshoot or steady-state oscillation when facing large-inertia, large-time-delay systems.
- “Drift and Lifespan” Dilemma of Temperature Sensors:
- Immersion Thermocouples: Operating long-term in high temperatures, strong electromagnetic interference, and highly corrosive aluminum or steel melts, thermocouple protection tubes are prone to dissolution and deformation, leading to distorted temperature readings.
- Infrared Pyrometers: Susceptible to dynamic changes in furnace smoke/dust, flame radiation, slag coverage rate, and metal surface emissivity, making it difficult to accurately capture the true internal temperature of the melt pool.
- Limitations of Multi-Zone Independent Regulation: Large induction furnaces often adopt single-loop or coarse-grained power regulation, failing to finely compensate for temperature differences across different depths and horizontal cross-sections of the melt pool.
IV. Engineering Breakthrough Pathways for Addressing Extreme Challenges
To overcome the aforementioned temperature control limits, the next generation of medium-frequency induction furnaces and heat treatment systems is evolving in the following directions:
| Key Technical Dimension | Traditional Temperature Control Method | Extreme Temperature Control Upgrade Pathway |
| Power Supply & Control Algorithms | Traditional fixed-parameter PID with lagging response | Introduction of fuzzy adaptive PID and neural network predictive control to match load impedance changes in real time |
| Electromagnetic-Thermal-Fluid Coupling | Reliance solely on empirical power settings | Integration of multi-physics (EMF-CFD) joint simulation to optimize coil turn distribution and stirring force fields |
| Sensing & Compensation | Single thermocouple or interference-prone infrared pyrometers | Multi-point distributed optical fiber temperature measurement + dynamic emissivity self-calibration + slag state visual recognition |
| Proseso & Hardware Synergy | Open-air or crude atmosphere regulation | Fully closed-loop inert gas protection / vacuum precision-pressure melting, combined with pulsed step heating |